
Twenty-two minutes, and the filter came out grey
A four-bed recovery bay, fourteen oxygen terminals off one riser, and a second-fix crew who purged every outlet for twenty-two minutes against a kitchen timer, because twenty-two minutes was the figure that had been written into the method statement on the last job. The verifier arrived on a Tuesday, put a particulate filter on the first outlet, and took off a disc the colour of a pencil rubbing. Eleven of the fourteen came off the same way. The gas had been flowing for twenty-two minutes at every one of them.
Time is the one quantity that does not appear anywhere in the mechanism. What leaves the pipe is a volume, and volume is flow multiplied by time, and the flow through a station outlet with a purge adapter clipped to it depends on the regulator setting, the restriction inside the adapter, the line pressure that morning and how many other outlets somebody left open two floors down. Twenty-two minutes on Monday and twenty-two minutes on Thursday are not the same purge, and neither of them is a measurement of what is still in the tube.
Two numbers and one signature decide this job. The volume of gas that has to pass, which is a multiple of the pipe's own internal volume and is an ordering quantity. The rate at which it has to move, which is set by the largest bore in the path rather than by the outlet you are standing at. And the test at the terminal, which is what the code accepts and which somebody other than the installing contractor performs. The arithmetic is easy. The part worth getting right is understanding what the arithmetic cannot tell you.
Four operations get called purging, and only one of them is a test
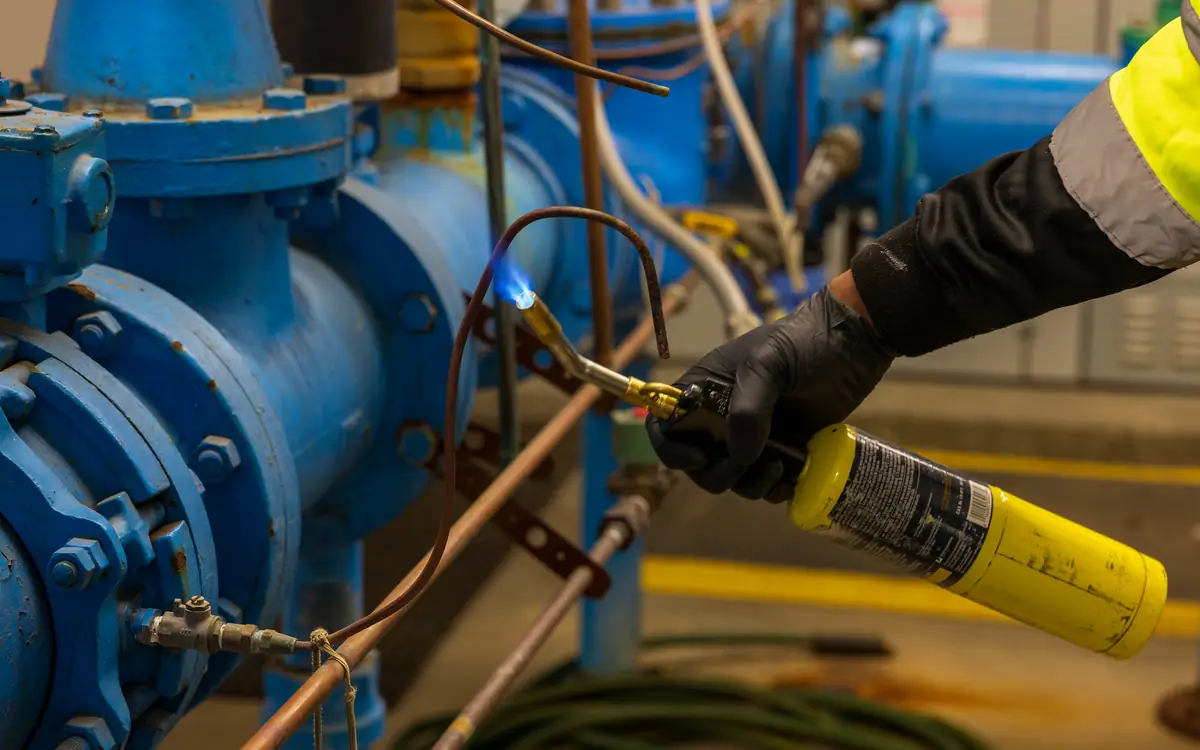
The first happens with a flame in your hand. Copper brazed in air grows a hard, black cupric oxide scale on the inside of the joint, and that scale flakes off later into the gas stream heading for a patient. NFPA 99 requires medical gas piping to be brazed under a continuous flow of oil-free dry nitrogen NF passing through the tube, with the far end open so the purge has somewhere to go. This purge removes nothing whatever. It prevents. The flow is a trickle — enough to hold the atmosphere out of the joint, and low enough that it does not pressurise the assembly and push filler metal back out of the capillary while it is still liquid.
The second is blowdown, and it is the violent one. After brazing and before any pressure test, the run is blown out with heavy intermittent bursts of nitrogen to drive swarf, filings, cut ends and the general dirt of a ceiling void toward the open ends. Bursts rather than a steady stream, because a chip resting in the invert of a horizontal main does not care about a settled flow profile; it moves when the transient hits it, or it does not move at all. This is the highest volumetric flow that pipework will ever see, and it is deliberately done before the system is closed up and tested.
The third is the purge at each terminal, with the gas of system designation rather than with nitrogen, once the pipework has passed its pressure and cross-connection tests. This is the one the volume arithmetic on this page is about. The fourth is not a purge at all: it is the verifier's particulate, purity and concentration testing, and it is the only operation in the list that produces an acceptance.
A method statement that says purge the system is therefore ambiguous across four operations that use two different gases, three different flow regimes and two different sets of hands. Name which one, every time it appears.
| Operation | Gas and flow | When | What it achieves |
|---|---|---|---|
| Brazing purge | Oil-free dry nitrogen NF, continuous trickle | Throughout brazing, with the run open at the far end | Keeps atmosphere off the inside of the hot joint so no oxide scale forms. Removes nothing — it prevents the contamination the other three have to chase. |
| Blowdown | Nitrogen, heavy intermittent bursts | After brazing, before the piping is pressure tested | Dislodges swarf, filings and construction debris using the transient rather than the settled flow, at the highest rate the run will ever carry. |
| Purge at each terminal | The gas of system designation, steady and metered | After the pressure and cross-connection tests have passed | Sweeps each branch with the gas that will actually run in it, one outlet at a time. This is the operation the volume multiple applies to. |
| Verification testing at the outlet | No purging — measurement only | By an independent verifier, before the system is handed over | Particulate, hydrocarbon content and gas identity checked against the acceptance criteria in the adopted code. The only step that produces a pass. |
The volume you sweep is a path, not a system
Internal volume is bore area times developed length, and the word that matters is bore. Medical gas copper in North America is ASTM B819 seamless tube, factory cleaned for oxygen service, capped, and dimensionally the same as ASTM B88 Type K and Type L — so nominal 1 inch Type L has a bore of 26.0 mm, not the 25.4 mm the label suggests, and Type K in the same nominal size has a thicker wall and a smaller bore again. In Europe the tube is BS EN 13348, supplied in metric outside diameters of 15, 22, 28, 35, 42 and 54 mm with wall thicknesses from the standard's own table. Take the bore off the tube certificate rather than off the size written on the drawing.
Now the trap that catches the estimate. You do not sweep a system; you sweep the path from the source to whichever terminal you have open. Gas leaves through one hole at a time, so a branch hanging off a tee with its outlet shut sees nothing but slow diffusion no matter how long the main beside it has been flowing. Purge terminal by terminal and the trunk gets swept once per terminal, while each branch gets swept once in its life. The gas that has to be bought is the sum over outlets of trunk plus that outlet's branch, which on a fourteen-outlet riser is several times the number a single system volume would suggest.
So the take-off is per branch with an outlet count against each. A worked zone: 40 m of 1-1/4 inch main at 0.811 L/m is 32.4 litres, 60 m of 3/4 inch distribution at 0.312 L/m is 18.7 litres, and 90 m of 1/2 inch drops at 0.151 L/m is 13.6 litres, so the zone holds roughly 65 litres in total while the longest single path through it — main, branch and drop — holds under 40. The path figure is the one that governs how long any single outlet takes. Neither of them is the order quantity: that is the path volume added up over every outlet you have to open, which is why the ordering line and the duration line come off the same take-off and never carry the same number.
Every zone also holds gas that nothing will ever sweep. A capped spur left for a future bed head, a dropper to a terminal that is drawn but not in this phase, the leg beyond a zone valve held shut through commissioning — each of those holds its own litres and none of them lies on the path to an open outlet. That is not a purging problem so much as a purging impossibility. Take them out where they can come out, and where they cannot, write down where they are, so that the person who commissions the next phase knows the spur behind that blank plate has never had gas moved through it in its life.
The velocity column below is there to make one point and is not a code requirement: 100 litres per minute is an arbitrary flowmeter setting, chosen because it is a plausible one, and the ratio across the column is the finding. The same setting that scours a half-inch drop at eleven metres per second barely stirs a two-inch main at under one.
| Nominal size | Bore | Litres per metre | US gal per 100 ft | Velocity at 100 L/min |
|---|---|---|---|---|
| 1/2 in | 13.8 mm (0.545 in) | 0.151 | 1.21 | 11.1 m/s |
| 3/4 in | 19.9 mm (0.785 in) | 0.312 | 2.51 | 5.3 m/s |
| 1 in | 26.0 mm (1.025 in) | 0.532 | 4.29 | 3.1 m/s |
| 1-1/4 in | 32.1 mm (1.265 in) | 0.811 | 6.53 | 2.1 m/s |
| 1-1/2 in | 38.2 mm (1.505 in) | 1.148 | 9.24 | 1.5 m/s |
| 2 in | 50.4 mm (1.985 in) | 1.997 | 16.08 | 0.8 m/s |
Work each leg from its bore and its developed length rather than from the table when the tube is Type K or EN 13348 metric. Type K holds less per metre than the Type L above; EN metric tube is a different set of outside diameters and wall thicknesses again, and in the larger sizes it holds more, not less.
The pipe's inside diameter, not the nominal or outside size.
The total length of pipe run.
Estimated pipe volume needed
0.7573 gallons
- Volume (liters)
- 2.87 liters
- Volume (cubic in)
- 174.95 cubic in
They open the calculator with your figures already in it
Pipe Volume Calculator: 0.7573 gallons — shown in imperial, US market. The link sets both, so the result they see is the one on your screen.
Estimated cost — your price
This site holds no price list for this material — local prices vary too much to publish honestly. Enter your supplier's price and the result is costed with it.
What this calculation does not cover
- The figure is the contents of a straight bore and nothing else. Fittings, valve bodies, meters, strainers and any water standing in a cylinder or tank at the end of the run are not counted, and the pipe wall is excluded — so this is not the volume of pipe material, and not the space the pipe occupies in a chase or trench.
- Volume scales with the square of the bore, so an inside diameter that is 9 per cent out produces a volume 19 per cent out. Published inside diameters differ by material, schedule and class for the same nominal size, and the calculator takes whatever figure you type at face value — it has no way of knowing that a half-inch pipe was entered at half an inch.
- It assumes the run is completely full of liquid over its whole length. Gravity drains, waste stacks and sewers are designed to flow part full, and a system that has not been purged holds air at its high points, so both contain less than this number says.
- It answers how much the run holds, not how long the wait is. Turning that volume into a hot-water delay needs the fixture's flow rate as well, and the real delay runs longer because the first hot water gives up heat to the pipe wall and to whatever surrounds it. No time calculation happens on this page.
- Nothing here is a sizing or a support check. Velocity, friction loss and pressure drop are separate calculations, and a long run that holds a comfortable volume can still be too small to deliver flow. The contents also weigh whatever that volume of water weighs, which bears on hanger spacing and is not assessed.
Why the multiple is five to ten and not one
If gas travelled down a pipe as a flat piston, one internal volume would clear it and the multiplier would be a superstition. It does not. The front smears from the moment it starts: centre-line gas outruns the boundary layer, every tee shears the two apart, every change of section stirs them back together, and what arrives at the outlet is a graded mixture rather than an edge.
The honest way to handle that is to bracket it. Perfect plug flow is the optimistic bound and needs one volume. Perfect stirring is the pessimistic bound, where the remaining fraction of the original atmosphere after n volume exchanges is e to the power of minus n: one exchange leaves 36.8 percent of the air still in there, three leaves 5.0 percent, five leaves 0.67 percent, seven leaves 0.09 percent and ten leaves 0.0045 percent. Real copper sits between the bounds and drifts toward the stirred end wherever the geometry stops being a straight run. That is the whole reason accepted practice lands on a multiple of five to ten rather than on one, and it is also why moving from five to ten buys an order of magnitude in residual rather than a factor of two.
What the multiplier is for is buying. It tells you how many litres of free gas to put on the order and how many cylinders have to be on that floor on the day. It is not a statement that the line is clean, and it cannot be, because the model behind it assumes the contaminant is a gas that mixes. Particulate ignores it completely. A copper flake sits exactly where it is through any number of volume exchanges until the velocity past it crosses the threshold that moves it, and then it moves all at once, which is why the code puts a filter on the outlet instead of a meter on the cylinder.
One unit trap sits in the ordering. The purge volume is free gas at atmospheric pressure, not litres of cylinder. A cylinder's free content is roughly its water capacity in litres multiplied by its fill pressure in bar, a few percent under that in practice because nitrogen is not ideal at 200 bar. The label on the shoulder carries both figures; use them rather than a remembered cylinder size, because the same physical bottle is filled to different pressures in different markets.
Feed it one path's volume for what a single outlet costs you, or the paths added up over every outlet for what has to be on the floor, with the multiple your procedure calls for. What comes back is free litres — a purchasing figure, not a pass.
The total internal volume of the medical gas pipeline being purged.
How many times the pipe's internal volume of inert gas is pushed through during the purge.
Nitrogen purge volume needed
25 gal
Confirm the exact purge multiplier and procedure required by NFPA 99 and your medical gas verifier for the specific system and commissioning requirements — this is a general estimating multiplier, not a substitute for the certified installer's commissioning procedure.
They open the calculator with your figures already in it
Medical Gas Pipeline Nitrogen Purge Volume Calculator: 25 gal — shown in imperial, US market. The link sets both, so the result they see is the one on your screen.
Estimated cost — your price
This site holds no price list for this material — local prices vary too much to publish honestly. Enter your supplier's price and the result is costed with it.
What this calculation does not cover
- The purge that dominates the nitrogen order is not this one. Every medical gas joint is brazed with nitrogen flowing continuously through the tube to stop copper oxide scale forming on the inside, and that flow runs for the whole of every brazing operation across the entire installation — governed by braze hours and flow rate, not by pipe volume. On a full pipeline it is normally several times the displacement purge computed here.
- The answer is free gas at atmospheric pressure, which is not what is inside the cylinder. Nitrogen arrives compressed, so a 50-liter cylinder at 150 bar holds roughly 7,500 liters (1,981 gal) of free gas — cylinder water volume times pressure in bar. Ordering bottles straight off this figure without that conversion brings either a truckload too many or one too few.
- Any nitrogen will not do. Purge and braze gas for a medical pipeline has to be oil-free dry nitrogen of the grade the standard names, because industrial and welding nitrogen can carry oil mist and moisture — and putting that through tube that will later deliver oxygen to a patient contaminates the system in precisely the way the particulate and purity tests at verification exist to catch.
Rate is a separate decision, and the biggest bore in the path sets it
Choose the flow for the largest section the gas has to cross, then accept that it is extravagant in the drops. A rate that keeps a 2 inch main moving fast enough to lift debris will roar through a 1/2 inch tail; a rate that feels right at the tail leaves the main almost static, which is precisely the condition under which a line flows for twenty-two minutes and stays dirty. Where a zone contains both, purge it in stages: the main from a capped end or a zone valve at a rate the main needs, and the drops afterwards at the terminals.
The terminal itself is a restriction, and a small one. A station outlet with a purge adapter on it will pass what the adapter passes at the line pressure available, and no more, whatever the regulator says. Check that figure before assuming an outlet is a convenient hole. If the rate the calculation asks for cannot be got through the adapter, the honest answer is to purge from somewhere else in the run and treat the terminal purge as the finishing sweep it actually is.
Steady flow and burst flow do different work and should not be swapped. A settled stream establishes its profile in the first second and then changes nothing about the forces on a particle lying still; a burst re-establishes the transient every time it starts. Blowdown is bursts, before the system is closed. The terminal purge ahead of the purity test is steady and metered, because there you are counting volume rather than shaking things loose.
Direction matters as much as rate. Work outward from the source, take one terminal at a time, close each behind you, and never open a branch you have already cleared while pushing gas past its tee. It is the same discipline as flushing a heating system and for the same reason: everything you dislodge goes somewhere, and the only acceptable somewhere is out of an open end.
- Confirm the tube is ASTM B819 or BS EN 13348 medical gas copper, that the caps were still on it, and that each cap came off at the moment of assembly rather than at the start of the week.
- Braze every joint under a continuous flow of oil-free dry nitrogen NF with the run open at the far end, using a filler metal to AWS A5.8 and no flux on copper-to-copper joints.
- Blow the run down with heavy intermittent nitrogen before any pressure test, working from the source toward the open ends.
- Pressure test the piping, then leave it standing for the period the adopted code requires, with the gauge read at the start and the end by the same person and both readings written down.
- Run the cross-connection test: drop every system to atmospheric, raise one gas at a time, and check every outlet of every system while it is up.
- Purge each terminal in turn with the gas of system designation, outward from the source, at a rate chosen for the largest bore in the path and for the volume multiple the procedure specifies.
- Present the outlets to the verifier for particulate, purity and concentration testing, and touch nothing in the pipework between the purge and the test.
- Make the tie-in last, then re-test and re-purge everything downstream of that joint before anybody uses it.
Three gauges, three unit systems, one number that has to be right
The nitrogen regulator on the floor is almost certainly graduated in bar. The manifold gauge is very likely psi. The specification will be in kPa. On a medical gas job those three sit within a few metres of each other and refer to the same physical quantity, and there is no cultural convention that saves you: the terminal pressure of oxygen, nitrous oxide and medical air is nominally in the 345 to 380 kPa band under NFPA 99 practice, which is the 50 to 55 psi people quote, while HTM 02-01 practice works to a nominal 400 kPa. Instrument air, surgical air and nitrogen for tool drive run considerably higher again. Take the figure off the project's own schedule, not off the last hospital.
Test pressures then stack a second layer on top. The initial pressure test is run at one and a half times the system working pressure, and the code also carries a floor beneath that multiple which should be read off the edition adopted on the job rather than remembered. The standing pressure test is a different pressure held for a stated period, and it is the one where a reading transcribed into the wrong unit produces a certificate that is wrong by a factor of seven. Vacuum is not on the same scale at all — mm Hg, inHg or kPa absolute — and a gauge reading zero means two entirely different physical states depending on which of those it is calibrated in. None of this is difficult, and all of it gets done at the end of a long day by somebody holding a torch in one hand, which is why the conversion is worth doing on the page, once, in front of whoever has to sign the sheet.
Convert the reading before it goes on the certificate rather than after, because a psi figure written into a kPa field survives as a document and is out by a factor of nearly seven.
The pressure value to convert.
The unit your starting value is in.
Converted pressure
206.8 kPa
They open the calculator with your figures already in it
Pressure Conversion Calculator (PSI ↔ kPa): 207 kPa — shown in imperial, US market. The link sets both, so the result they see is the one on your screen.
Add the equipment this sizes
This result is a specification — 206.8 kPa — not a quantity. Put the thing it sizes into your project: how many, what you call it, and your supplier’s price.
What this calculation does not cover
- The conversion changes the unit, not the reference datum. Almost every dial on a compressor, pressure tank or tyre reads gauge pressure, so 30 PSI converts to 206.84 kPa gauge, which is about 308 kPa absolute once the 101.325 kPa of atmosphere at sea level is added. A spec sheet quoting kPa(a), bar(a) or psia is describing a different quantity, and this page will not shift a reading between the two scales.
- Only PSI and kilopascals are offered, so a figure quoted in any other pressure unit has to be brought into one of those two first. One bar is 100 kPa and one MPa is 1000 kPa, both exact; a gas appliance figure in inches of water gauge is a far smaller unit, at roughly 249 Pa or 0.036 PSI per inch, and reading such a figure as PSI overstates it by a factor of about 28.
- Pressure is not head, and no fluid property enters this arithmetic at all. The same factor is applied whether the reading came from air, water or hydraulic oil, whereas converting pressure to a height of liquid depends on density, so one PSI is about 2.31 feet of water column only for water at ordinary temperatures. Use the PSI to feet of head calculator rather than reading this result as a lift.
- A converted figure says nothing about whether the pipe, hose, fitting or vessel is rated for it. Pressure ratings are also derated as temperature rises, sharply so for plastic pipe, and this page has no material or temperature input, so a result inside a component's cold rating can still exceed what that component may carry hot.
Verification is a measurement at the terminal, and it is not your signature
NFPA 99 splits this work in two on purpose. The installing contractor carries out its own tests — blowdown, initial pressure test, cross-connection test, terminal purge and a standing pressure test — and then a separate party, technically competent, experienced and independent of the installer, verifies the system before it is used. The competency route in North America runs through the ASSE Series 6000 qualifications: 6010 for the installer and brazer, 6020 for the inspector, 6030 for the verifier and 6040 for maintenance personnel. The independence is not administrative fussiness. The person who buried the pipe is the worst available witness to what is inside it.
What the verifier actually does is a list of measurements, and it is worth reading the list because none of the entries is a duration. Standing pressure. Cross-connection. Valve operation. Alarm operation. Flow and operational pressure at the terminal, which is where a run that was sized optimistically finally admits it. Particulate at the outlet through a filter. Purity, meaning hydrocarbon content and moisture. And the concentration test with a calibrated analyser at every terminal, which is the only test in the sequence that proves what gas is in the pipe rather than how clean it is.
The acceptance criteria live in documents, not in anybody's memory, and they differ. NFPA 99 references the United States Pharmacopeia monographs for the gas concerned. The United Kingdom works to HTM 02-01 Part A and the European Pharmacopoeia, with the pipeline standard BS EN ISO 7396-1 underneath it. Australia and New Zealand work to AS 2896, Canada to CSA Z7396.1. The numbers in those documents are not interchangeable, which is exactly why this page does not print any of them: a ppm limit that is correct in one is quietly wrong in another, and a wrong limit on a hospital job is worse than no limit at all.
Which brings the argument back to the timer. Elapsed time is not expressed in any unit the acceptance criteria are written in. It is not litres, it is not parts per million, it is not percent oxygen and it is not a particulate count. A record that reads purged twenty-two minutes is evidence that a person stood at an outlet, and nothing else. A record that carries a filter disc, an analyser reading and a signature from somebody who does not work for you is evidence about the pipe.
Flow proves nothing at all about identity
There is a failure mode that a flowing line hides completely, and it is the reason the cross-connection test exists rather than being an optional refinement. An outlet labelled oxygen, fed from a manifold, delivering full line pressure to a probe that clicks home correctly, presenting every symptom of a working terminal — and carrying the wrong gas. Nothing about flow, pressure or duration distinguishes that outlet from a correct one. Only an analyser does.
It happens through ordinary means. Two runs brazed in the same ceiling on the same afternoon and the labels transposed at second fix. A temporary jumper installed to keep a ward running during a phase and never taken out. A zone valve fed from the wrong header at a plant room that was re-arranged after the drawings were issued. A terminal unit block fitted with the wrong gas-specific insert. The keying systems — DISS connections to CGA V-5 in North America, NIST and probe indexing to BS EN ISO 9170-1 elsewhere — protect the connection between the equipment and the outlet. They do nothing about which pipe is behind the wall plate.
The test is unglamorous and slow: reduce every system in the building to atmospheric pressure, raise one gas at a time to its operating pressure, and walk every outlet of every system with an analyser while that one gas is up. Then the verifier's concentration test at the end catches anything the first pass did not. Both of them are done at the terminal, which is the recurring point of this whole page — the only place any of this can honestly be measured is where the gas comes out.
The tie-in undoes the certificate, and the paperwork outlives everyone
New pipework is almost always verified in isolation and then connected to a system that is already running, and the moment that joint is made, the certificate you were holding describes something that no longer exists. The tie-in joint itself is unverified by definition, the section either side of it has been opened to atmosphere, and everything downstream is now fed from a source nobody tested as part of this package. NFPA 99 has a final tie-in test for exactly this, and it is the step most often compressed when a programme is late. Purge and test again, downstream of the joint, before anybody uses an outlet.
In an occupied hospital the tie-in is not a brazing problem, it is a clinical one. It needs a shutdown window, cylinder backup staged in the affected departments, a named person on the ward side who owns the decision to go, and a permit that says who may reopen the valve. The brazing takes twenty minutes; the arrangements around it take weeks, and phasing work in a live building has its own discipline that this page defers to rather than repeats.
What survives all of it is the record: the zone valve schedule, the outlet register with a line per terminal, the pressure and standing test sheets, the verifier's report, the certificate for the nitrogen used to braze and blow down, and the brazer's qualification. Four years later, when somebody adds two terminals to a bay and wants to know which header that riser comes off, that folder is the only thing that answers. Assemble it as the work happens, because reconstructing it afterwards means opening ceilings.
Before the first cap comes off the tube
What has to be settled before purging is planned, seeded with the 65-litre zone from the worked example and a purge multiple of six. That seed is the zone's own held volume, not an order quantity — replace it with the path volume summed over the outlets you have to open, and the multiple with the one your project procedure names.
- Bore from the tube certificate, not the size on the drawing — ASTM B819 Type K and Type L hold different volumes per metre in the same nominal size, and EN 13348 metric tube differs again. Volume is the one thing the label cannot tell you.
- A branch-by-branch volume with an outlet count against each — You sweep the path to the terminal that is open, so the trunk is swept once per outlet and each branch once in its life. The order quantity is the sum over outlets, not the system volume.
- Oil-free dry nitrogen NF, with its certificate of analysis — The brazing purge, the blowdown and the pre-test sweep are three separate draws on the same supply, and only the first of them runs for the whole duration of the pipework.
- The rate the largest bore in the path needs, and what the outlet adapter will actually pass — If the adapter cannot deliver it, purge from a capped end or a zone valve instead of pretending the terminal is a large hole.
- Which gauge, in which unit, at which stage — Line pressure, initial pressure test, standing pressure test and vacuum are four different readings on three unit systems. Convert once, in front of whoever signs.
- A verifier booked, independent of the installing contractor — ASSE 6030 in North America. Book the date before second fix, because a late verifier stops a handover as effectively as a failed test.
- A tie-in plan with a shutdown window and a named clinical owner — Cylinder backup staged, permit written, and the re-test and re-purge of everything downstream of the joint priced into the programme rather than discovered in it.
Opens the calculators above on one screen with the dimensions from this article already filled in. Quantities only — this site publishes no price list, because local prices vary too much to publish honestly.